If you’ve ever wondered about the differences between water-resistant, water-repellent, and waterproof textiles and clothing, you’ve come to the right place.
The main function of outdoor clothing is to protect you from the elements. In wet environments, the basic requirement is to keep the wearer dry. Therefore, the outer layer of your clothing, along with your gloves or mitts, needs to effectively resist moisture. But what do these terms actually mean? Is there a real difference between them? Here, we’ll answer these questions and break down the key distinctions between water-repellent, water-resistant, and waterproof fabrics..
When in contact with water, water-repellent materials cause moisture to bead up on the surface, allowing it to be easily shaken or wiped off. This means water cannot easily penetrate the material; however, with prolonged exposure or under higher pressure, the fabric will eventually “wet out” and absorb water. Water-repellency is typically achieved through compact textile structures or, more commonly, by treating fabrics with hydrophobic chemicals (like a DWR finish). Although “water-resistant” and “water-repellent” are often used interchangeably in marketing, there is a technical difference: water-repellent refers to the surface treatment that causes beading, while water-resistant refers to the fabric’s inherent ability to resist water penetration for longer. True waterproofing, on the other hand, is defined as a material’s ability to remain completely impervious to water, preventing any fluid penetration under normal conditions.
There are two primary methods for measuring the waterproofness of fabric. The first one simulates rain, while the other subjects the fabric to hydrostatic pressure (known as the hydrostatic head test). The minimum hydrostatic pressure at which a fabric is generally considered “rainproof” is 5000 mm. For a material to be classified as fully waterproof, its hydrostatic head rating typically reaches 10,000 to 15,000 mm. This means a column of water would need to reach a height of 10 to 15 meters over a specific point on the fabric before any water begins to leak through. For materials designed for harsh, extreme conditions, waterproof ratings usually fall between 15,000 and 30,000 mm. Fabrics in this range are completely waterproof and will not leak, even under a heavy downpour or the sustained pressure of a heavy backpack.
Table 1: Fabric waterproof ratings

Source: evo.com
The main challenge when using waterproof fabrics in garments is wearer comfort. In the past, waterproof technologies relied mainly on coating or sealing the textile substrate, effectively blocking its pores. While this created a solid barrier against environmental moisture, it also restricted perspiration from escaping the body. This led to moisture accumulation and condensation inside the clothing, which, as a result, sharply decreased the garment’s insulating ability. Therefore, moisture vapor transfer must be managed in both directions: keeping external water out while allowing internal vapor to escape.
Human skin releases moisture continuously, both at rest (insensible perspiration) and during physical activity (sensible perspiration). Because of this, the moisture vapor produced by the body must be effectively vented. This challenge is solved by waterproof breathable textiles. These advanced materials allow water vapor to escape through the fabric while blocking liquid water, reducing overheating and sweat buildup to keep the skin drier and more comfortable.

Table of Contents
Water-repellent vs water-resistant vs waterproof: history
First attempts
The earliest recorded attempts to create water-repellent protective clothing date back to the 15th century. At that time, sailors and fishermen began treating their garments with animal fats, fish oils, and wax to block out the elements. While it is difficult to measure the exact success of these rudimentary methods, they laid the crucial groundwork for future innovations. The first truly patented waterproof fabric, however, arrived roughly 400 years later. In 1823, Scottish chemist Charles Macintosh patented a revolutionary process that used dissolved rubber to seal fabric. While this process would be refined over time, Macintosh’s invention was far superior to any other waterproofing solutions available on the market.
Rubber vulcanization and the first waterproof fabric for coats
By sandwiching a layer of liquid rubber (made with an oily liquid by-product of tar called naphtha) between two woven fabrics, Macintosh created a new material that was resistant to water while also remaining flexible and wearable. Resistant to rainy weather and wet conditions, the new fabric was perfect for making coats. However, there were some problems with this fabric caused by the use of unstable rubber. These problems were eliminated when a more stable material was produced thanks to the process of rubber vulcanization, patented in November 1843 by Thomas Hancock in England, and later in 1844 by Charles Goodyear in the United States.
Despite the fact that rubber is a good material for waterproofing, there is a significant problem with using rubberized textile fabrics for clothing. The downside of these garments is that they present a barrier to the evaporation of sweat, and this very limited water vapor transfer leads to overheating of the wearer’s body. As a result, sweat vapors condense in contact with the interior surface of the clothing and accumulate in the textile layers in direct contact with the skin. The result is a wearer who is wet with perspiration and highly uncomfortable. Thus, as far as the wearer’s comfort is concerned, having a waterproof fabric is just half of the solution. The other half is called breathability, or moisture vapor permeability. Combining these two properties, the first waterproof breathable fabrics were produced.
First modern waterproof/water-resistant breathable fabric
The first real waterproof breathable fabric was produced in England during World War II (mass production started in 1943). A densely woven, breathable fabric called Ventile, it is made from 100% cotton, utilizing high-quality long-staple fibers. It was originally meant to replace flax in garments for military applications.
SSo, how does this fabric function? When the fabric comes into contact with water, the cotton fibers swell, the size of the pores between the yarns decreases, and the interstices within the fabric close up, preventing further passage of water. Moreover, the fabric is typically treated with a DWR (durable water repellent) finish, which enhances the water-resistant properties of the material.
Ventile is now used for outdoor sportswear in activities such as mountaineering, trekking, and nature watching, because the fabric provides excellent protection against wind, rain, snow, and cold. Additionally, Ventile is suitable for use in extreme and hostile environments. For example, it is used on Arctic, Antarctic, and Himalayan expeditions. It seems that cotton doesn’t always kill…
Gore-Tex and the rise of the waterproof breathable membranes
The first microporous ePTFE (expanded polytetrafluoroethylene) membrane was created by Wilbert L. Gore and his son, Robert W. Gore. In 1969, thanks to a happy accident (instead of slowly stretching a heated PTFE rod, he applied a sudden yank, and it stretched 800%), Robert Gore created this new material. The first Gore-Tex materials appeared on the market in 1976, starting a revolution in the concept of waterproof breathable clothing. This membrane has approximately 1.4 billion pores per square cm (9 billion pores per square inch), with each pore being 20 000 times smaller than a drop of water. The waterproof, breathable, microporous membrane introduced by Gore holds an important place in the performance sportswear market.
Since the mass production of waterproof clothes with Gore-Tex material started some 50 years ago, there have been many developments in waterproof breathable fabrics.
Water-repellent textiles are obtained using specific hydrophobic finishing treatments. Thanks to impregnation with these treatments, water-repellent fabrics offer light rain resistance.

Droplets can bead on all kinds of water-resistant fabrics
The most frequent use of such fabrics is in the clothing industry. Due to the complex requirements of users (protection, comfort, functionality, etc.), waterproof fabrics must possess a combination of properties that ensure the multifunctional characteristics of the garment. The performance level of waterproof and water-repellent materials used for clothing is determined by two groups of factors:
- Subjective variables: Related to the requirements and comfort level of the final user.
- Objective variables: Related to environmental conditions, risk factors, and the specifics of the activities carried out by the user.
Waterproofness is a requirement imposed mainly by the environment (especially weather conditions) and is related to the behavior of textile materials toward water. Generally, textile materials can be divided into:
- Materials that absorb and retain water, known as hydrophilic materials.
- Materials that repel water, known as hydrophobic materials.
Waterproof fabrics
If you need to stay completely dry in driving rain or snow, your best option is to wear a properly designed garment made from waterproof breathable fabric, featuring waterproof zippers, sealed seams, and virtually no openings through which water can penetrate.
Conventional waterproofing treatments work as follows: by covering the pores with a layer of polymer or a membrane, fluids cannot pass through the textile material (while the outer water-repellent finish helps maintain breathability by preventing the face fabric from soaking up water).
Depending on their structure and/or the technology used, waterproof materials are either:
- Inherent waterproof materials; or
- Textile materials with waterproofing finishing treatments.
Waterproof materials are generally created using surface finishing treatments. “Covering” is a general term referring to the application of one or more layers of an adherent polymeric product to one or both sides of a textile material. In this way, a polymeric film is formed on the surface of the textile.
Two main technologies are used:
- Coating technology, where the polymer is applied via direct layering or impregnation. The polymer is usually in the form of a paste or a high-viscosity liquid. Such coatings are extremely thin, typically in the range of 10–100 μm.
- Laminating technology, which involves bonding a separate layer (such as a membrane or foam) to the surface of the textile material. The membrane itself is very thin (e.g., around 10 μm for ePTFE), so the final thickness of the applied film generally remains in the 10–100 μm range.
Coated
During impregnation, a solution or a low- or high-viscosity polymer dispersion is deposited uniformly on the entire textile surface using different processes. A general characteristic of impregnated materials is that the components cannot be clearly separated because the polymer is dispersed among the structural elements of the textile. The finishing technology can cover either one side of the material or both sides (this is called total impregnation). Nowadays, the most widely used coating substrate (textile) is polyester because of its dimensional stability, shrink resistance, and relatively low price.
Laminated
Laminated waterproof materials are multicomponent products (two or more layers, one of which is the textile fabric) requiring bonding by the use of:
- A special adhesive added to the polymer (solutions in organic solvents, powders, granules, or fibers); and
- The inherent adhesive properties of one or more component layers (membranes, foams, or expanded foils).
Natural (primarily rubber) and synthetic polymers are suitable for laminating textiles. Although the range of synthetic polymers is relatively wide, approximately 90% of the synthetic polymers used for laminating textile materials are polyurethanes.
The morphological structure of the coated and laminated materials, along with the nature of the polymers, is important, as these are key factors in obtaining a perfectly sealed waterproof product. The morphological structure of these materials includes:
- The number of layers that make up the coated or laminated waterproof material and their relative position in the garment.
- The absence or presence of pores (compact or porous layer) and the absence or presence of other added substances.
- The structure of the textile substrate (woven, knitted, or nonwoven fabrics) and any different finishing treatments applied to it.
Considering their position in the garment, the coated or laminated waterproof materials can be:
- With the covering layer towards the exterior: Mainly materials covered with elastomers and some materials laminated with compact foils. These materials are recommended for chemical protection and protection against particles.
- With the covering layer towards the interior: Used mainly for laminated materials with a membrane or film that has low mechanical strength. For increased durability, the polymeric film is covered with a hydrophilic polyurethane (PU) layer and/or a thin textile fabric. These materials are designed for wet weather protection.
Gore’s expanded PTFE membrane is often regarded as the starting point of commercially available high-performance waterproof breathable membranes. Initially, an ePTFE membrane claiming 90% void volume was laminated to a support fabric; however, the pores became contaminated by sweat or detergents, thus reducing overall breathability. To overcome this drawback, a thin hydrophilic polyurethane coating was applied to the body side of the membrane to prevent contamination (known as 2nd generation Gore-Tex).

Here you see a comparison between the old and the new version of GORE-TEX Pro. On top is the face fabric in red color, in gray/white is the ePTFE membrane, and the grey strands just below the membrane depict the lining. In the new version, the white PU layer has been replaced by the thin gray ePTFE “sandwich”.
Source: evo.com
Water-repellent fabrics
Water-repellent textiles usually resist wetting when worn in intermittent rain but do not provide adequate protection against driving rain. Unlike waterproof fabrics, water-repellent textiles have open pores, making them permeable to air, water vapor, and liquid water (at high hydrostatic pressure). In order to obtain a water-repellent fabric, a hydrophobic material is applied to the fiber surface. As a result of this procedure, the fabric remains porous, allowing air and water vapor to pass through. A downside is that in extreme weather conditions, the fabric will eventually leak.
The advantage of hydrophobic textiles is enhanced breathability; however, they offer less protection against water. Water-repellent fabrics are used mainly in the production of conventional clothing or as an exterior layer of waterproof clothing. The hydrophobicity can be either durable (long-lasting, due to the application of water repellents, DWR) or temporary.
There are two groups of water-repellent textiles:
- Inherent water-repellent textile materials.
- Textile materials finished with water repellent.
Water repellency is specific to compact textile structures. Thus, inherent water-repellent materials are (a) high-density woven fabrics, made of very fine yarns and filaments, and (b) nonwoven materials.

The invention of water-resistant breathable fabrics was welcomed by outdoor lovers from all over the world
The hydrophobization of textile materials is achieved by using different chemicals. These substances orient their hydrophobic groups towards the textile fibers, thus forming a protective brush against water. The hydrophobization agent applied to the surface of the garment allows water drops to maintain their shape without spreading onto the fibers. In general, the main limitation of water-repellent treatments is the fabric’s inherent surface porosity.
Hydrophobization can be achieved through the use of several technologies and/or materials. The main types are the following:
- Hydrophobization with additives (aluminum organic salts, aluminum soaps, paraffin emulsions with aluminum salts).
- Hydrophobization with resin-type reactive agents.
- Hydrophobization through chemical modification of the fibers.
- Textile finishing with nanoparticles. Oleophobization techniques give textile materials the property of repelling oils, thus creating protection against dirt and smudges while increasing the hydrophobization effect. Fluorocarbon resins are often used as oleophobization agents.
- Plasma treatment of the textile materials; plasma polymerization or plasma depositing of organic-silicone polymers can give a hydrophobic character to materials that are typically not hydrophobic (like cotton, for example).
The traditional technology used for producing water-repellent textiles requires a huge amount of water. This is related to two problems: 1) water pollution, and 2) high energy consumption. In contrast, plasma treatment does not require these large volumes of water or wet chemicals, nor does it require the large amount of energy needed to dry the fabric.
Textile materials are valuable thanks to properties like strength, flexibility, and low weight. Moreover, other properties adding more functionality, such as hydrophobicity, oleophobicity, or antibacterial activity, further increase their value. However, few textiles are inherently water-repellent, and none are oil-repellent. Traditionally, the water repellency of textiles is achieved by the application of functional chemicals, followed by careful drying. Some of these chemicals include metal salts, pyridinium-based finishes, silicone finishes, and fluorocarbons. Among them, only fluorocarbon finishes can repel both oil and water.
Water-resistant fabrics
The term “water resistance” describes the degree to which water droplets are able to wet and penetrate a fabric. Some people use the terms water-resistant and water-repellent interchangeably, while others argue that water-resistant and waterproof are the same. Actually, rain-resistant fabrics, also known as water-resistant, are in-between water-repellent and waterproof textiles.
Water-resistant fabrics and clothes are supposed to keep you dry in light to moderate rain. So, they provide better protection against rain and snow than water-repellent textiles. However, in prolonged wet weather, garments made of water-resistant textiles cannot protect you for too long, as they will eventually allow water to leak through. In bad weather, this makes them less reliable than waterproof breathable clothes and gear (which are resistant to higher hydrostatic pressure).
If we compare the three types of water-shedding fabrics, water-resistant textiles are much more similar to waterproof than to water-repellent fabrics, as, unlike the latter, they can repel moisture even without being treated with a hydrophobic finish. This means that water resistance implies an inherent ability of a fabric to ward off water. The degree of water resistance is measured by using a hydrostatic pressure test, so, technically, waterproof textiles are water-resistant as well (note that the opposite isn’t always true). Rain-resistant fabrics should be able to withstand a hydrostatic pressure of at least 1500 mm water column.
Rain-resistant clothes are often made from tightly woven man-made fabrics such as ripstop polyester and nylon. Other densely woven fabrics, such as taffeta and even cotton, are also readily used for manufacturing water-resistant clothing and gear.
Comparison
The table below illustrates the main features of water-repellent, waterproof, and waterproof breathable fabrics.
The main advantage of water-repellent textiles is their inherent breathability. This makes them suitable for manufacturing outdoor clothing that ensures comfort for the wearer. Additionally, they are less expensive than waterproof and waterproof breathable fabrics.
Waterproof fabrics are more resistant to wetting than water-repellent textiles and cheaper than waterproof breathable fabrics; however, these are their only advantages. In fact, they have several disadvantages in comparison to the other two materials. For this reason, they have largely been replaced by waterproof breathable fabrics in the production of outdoor clothing.
Waterproof breathable materials are expected to prevent the passage of water and air while ensuring the wearer’s comfort, even during activities in extreme weather conditions. Thus, waterproof breathable materials are waterproof, windproof, and relatively breathable. Their biggest disadvantage is their higher price.
Table 2: Features of waterproof, waterproof breathable, and water-repellent materials

Source: Waterproof and Water Repellent Textiles and Clothing
Below, you can see and compare some popular outdoor jackets with various levels of water resistance varying from water-repellent to rainproof to fully waterproof (from left to right, with a waterproof rating if available).

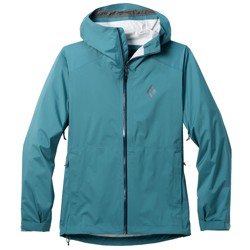
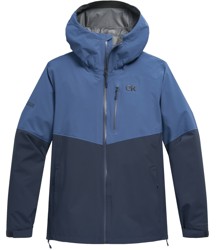
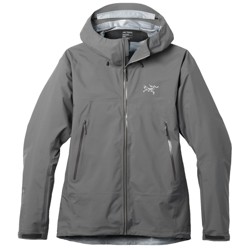
KUHL The One Hoody | Black Diamond Fineline (10K) | Outdoor Research Foray 3L (20K) | Arc’teryx Beta SL (above 20K)
While the level of water resistance of the jackets above varies, each one of them combines a multitude of other useful features.
Applications of waterproof, water-resistant, and water-repellent textiles
Waterproof, water-resistant, and water-repellent fabrics are quite popular for manufacturing both outdoor and indoor products. Unsurprisingly, the main use of such textiles is for clothing and gear (boots, backpacks, tents and shelters, sleeping bag covers, umbrellas, fasteners, and ponchos) for outdoor activities like hiking, backpacking, winter sports, etc. They are also used in household products such as bed covers, sheets, pillow protectors, garden furniture covers, pet blankets, etc.
 Want a lightweight shell jacket to protect you against the elements while living an active life? Then look for a versatile rain jacket with attractive features. Designed to provide a dry and comfortable outdoor experience, the Patagonia Torrentshell 3L is a great all-around rain jacket that offers full water and wind protection on and off the trail. It’s stylish and well-made, but more importantly, it’s easy to pack and can be used as both a rain jacket and a windbreaker during hiking excursions, fishing trips, and other outdoor activities. It performs well in cool and transitional weather, and the cut fits well even when wearing additional layers underneath for more warmth in winter. |
See the Men’s Torrentshell 3L on REI See the Women’s Torrentshell 3L on REI
Waterproof, water-repellent, and water-resistant textiles are also utilized in agriculture, architecture and construction, medicine and healthcare, and various other industries. Wheelchair cushions, stretcher covers, surgical garments, multilayer wound dressings, tree shelters, textile membranes for roofs, car covers, and protective clothing are just a small fraction of the applications for these fabrics. See our article on waterproof breathable fabrics for a comprehensive list of applications.

Hiking with an umbrella can be fun no matter where you are
Conclusion
In addition to protection from weather conditions like rain and wind, breathability is expected from sportswear. That’s why water-repellent or waterproof/water-resistant breathable fabrics are preferred.
Water-repellent fabrics are coated with a finish (such as DWR) that is resistant but not impervious to penetration by water, so water-repellent clothes will keep you dry for a relatively short time when walking in the rain. Thus, water-repellent clothes will provide some protection against intermittent rain but are not suitable to be worn in a downpour or in prolonged rainy weather. The biggest advantage of water-repellent pants and jackets is their breathability combined with some degree of water resistance.
Waterproof breathable fabrics are impervious to water and provide moisture vapor transfer from the inner side to the outer side of the material. They prevent the penetration and absorption of liquid water from the outside while allowing water vapor to be transmitted to the outside of the fabric. Waterproof breathable fabrics try to tackle the paradox of protection versus comfort. To some extent, they are doing well, as waterproof breathable textiles provide good protection and better thermal comfort in a cold and wet environment.
Functional clothing and moisture management principles have gained more and more popularity among people of all ages and occupations in the last 30-40 years. Thus, companies and researchers have had an incentive to develop the technology for manufacturing waterproof and water-repellent fabrics further. Well, the technology is still far from perfect, but it’s getting better.
Do you often use rain gear? If so, what type of gear do you prefer: water-repellent, waterproof, or water-resistant? Drop us a line in the comments section below.
Related Articles
All About Waterproof Breathable Fabrics
Guide to Waterproof Breathable Clothes
Ultimate Guide to Hiking Clothing
Like this post? PIN ME!!

What is the difference between water-proof & wind stopper? Which one has 3 layers of fabrics? Please advise. Thanks so much.
Hi,
Waterproof breathable or rain jackets are usually laminates that have 2, 2.5 or 3 bonded layers. So when you hear or read about a 3-layer jacket it is a waterproof breathable jacket. Generally, such construction consists of:
1) durable face fabric treated with a water-repellent finish
2) waterproof breathable membrane
3) lining
Waterproof jackets work best for wet conditions/changing weather. If rain is expected, a waterproof jacket is a good choice. Fully waterproof jackets can keep you dry for hours. We have a fantastic article about waterproof breathable clothing where we delve deeply into this (https://camotrek.com/blogs/news/waterproof-breathable-clothes/)
On the other hand, wind stoppers work best for windy weather. They are simpler constructions than rain jackets. Wind stoppers are often only water-repellent (not waterproof) thanks to a DWR-treatment and are more breathable than waterproof jackets. This makes them preferred for dry weather or when you expect only light rain so that your garment doesn’t soak with water. Thus wind stoppers are more versatile than waterproof breathable jackets but really both have their merits.